Austenitic 304 and 316L stainless steels work-harden the moment a standard hole saw, step drill, or jigsaw blade heats the edge. For UL 508A panel shops and OEM machine builders, modifying a blank stainless enclosure on the shop floor burns costly carbide tooling, distorts thin 16/14 ga doors, leaves jagged burrs that compromise HMI gaskets, and scatters conductive stainless shavings near PLC I/O terminals. The N4X-CNC-CUT panel-ready program shifts every aperture to nitrogen-assist CNC fiber-laser cutting prior to forming, welding, passivation, and robot-poured polyurethane gasketing.
What Can Be Fiber-Laser Cut Before Shipment
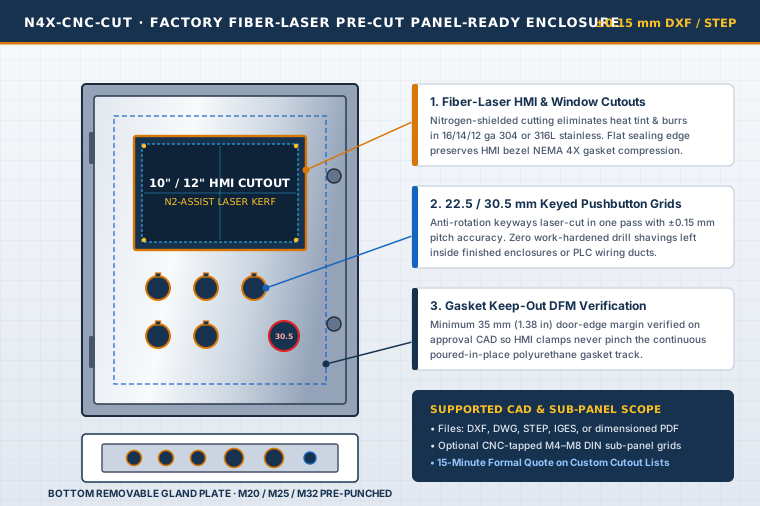
Our CNC fiber-laser fabrication workflow applies across any wall-mount or free-standing 304 or 316L cabinet platform at ±0.15 mm (±0.006 in) positional accuracy:
- HMI Touchscreen & Operator Windows: Exact rectangular cutouts and corner radii for Siemens, Allen-Bradley PanelView, Weintek, Red Lion, and Unitronics displays (for example 193 × 125 mm or 255 × 185 mm apertures) with mounting-clamp perimeter verification.
- 22.5 mm & 30.5 mm Pushbutton Arrays: Circular holes with integrated anti-rotation keyway notches cut in a single continuous pass so selector switches and E-stops never twist under gloved operation.
- Removable Cable Gland Plates: Pre-punched bottom or side stainless plates for M16–M63 metric or 1/2-in to 2-in NPT washdown cord grips with EPDM perimeter seals.
- Closed-Loop Thermal Unit Cutouts: Precise side-wall supply/return openings and threaded stud patterns for NEMA 4X enclosure air conditioners or air-to-water heat exchangers.
- Pre-Tapped Mounting Sub-Panels: Optional CNC-drilled and tapped M4–M8 grids on 12 ga or 10 ga galvanized sub-panels matching EPLAN or AutoCAD Electrical panel layouts.
Why Nitrogen-Assist Fiber Laser Preserves Corrosion Resistance
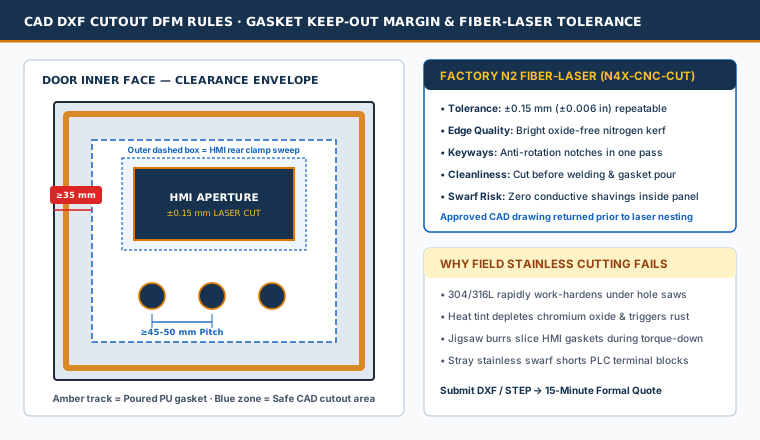
Oxygen-assisted thermal cutting leaves a dark iron-oxide scale along stainless steel edges that traps moisture and rusts inside washdown plants. Nitrogen-assist fiber-laser cutting shields the molten kerf with inert gas, leaving a bright, silver, burr-free edge that maintains chromium-oxide passivity right up to the HMI or pushbutton rubber seal. Because cutting occurs on flat stainless blanks before bending and robot-dispensed polyurethane gasket pouring, the finished cabinet arrives clean and ready for immediate DIN-rail population.
CAD Submission & 15-Minute Formal Quotation Workflow
| Stage | Customer Input | Engineering Desk Output |
|---|---|---|
| 1. Brief & File Upload | 2D DXF/DWG, 3D STEP, or dimensioned PDF + alloy (304/316L) & quantity | Formal engineering quotation delivered within 15 minutes |
| 2. DFM Clearance Check | HMI model codes, disconnect handle brand, gland entry counts | Verification of ≥35 mm gasket keep-out margin & clamp sweep |
| 3. Approval Drawing | Review flat-pattern cutout coordinates & sub-panel hole grid | Signed CAD freeze prior to laser nesting and welding |
| 4. Fabrication & Docs | Built to NEMA 250 Type 4X and UL 508A enclosure design requirements | Material mill certificates (304/316L) and ingress test reports available per project |
Sizing Tools & Cutout Preparation Checklists
- Estimate imperial dimensions, internal volume, and surface area before freezing your layout with our interactive NEMA 4X Sizing & Alloy Calculator.
- Avoid common door-clamp and gasket collisions by reviewing the UL 508A Stainless Cutout Drawing Checklist.
- Ready to convert your CAD drawing into panel-ready stainless hardware? Submit your parameters for a 15-Minute Formal Quote.
Standard & Custom-Engineered Models
Laser Pre-Cut HMI/Pushbutton Panel-Ready Enclosure
Custom-modified 304 or 316L wall-mount or floor-stand NEMA 4X enclosures with ±0.15 mm CAD fiber-laser HMI, pushbutton, louver/cooler, and gland plate cutouts.
Full Datasheet →